


An Ingredients Vibratory Hopper is a type of material handling equipment that delivers a precise, continuous and constant flow of ingredients into food processing, packaging or manufacturing machinery. The Equipment is designed to deliver an efficient flow of material to downstream processing and packaging machinery and eliminate manual handling and reduce product waste.
To ensure consistent ingredient feed for product quality and production efficiency, many modern facilities utilize the Ingredients Vibratory Hopper, a material handling solution that uses vibration to store, meter and convey bulk or free-flowing ingredients throughout the processing facility. Furthermore, it prevents clogging, bridging, and erratic discharge, thus enabling the free flow of material from the hopper to a conveyor, weigher, filler, or mixer.
Such a system is commonly used in food processing, pharmaceuticals, chemicals, and nutraceuticals, where precision, cleanliness, and reliability are paramount.
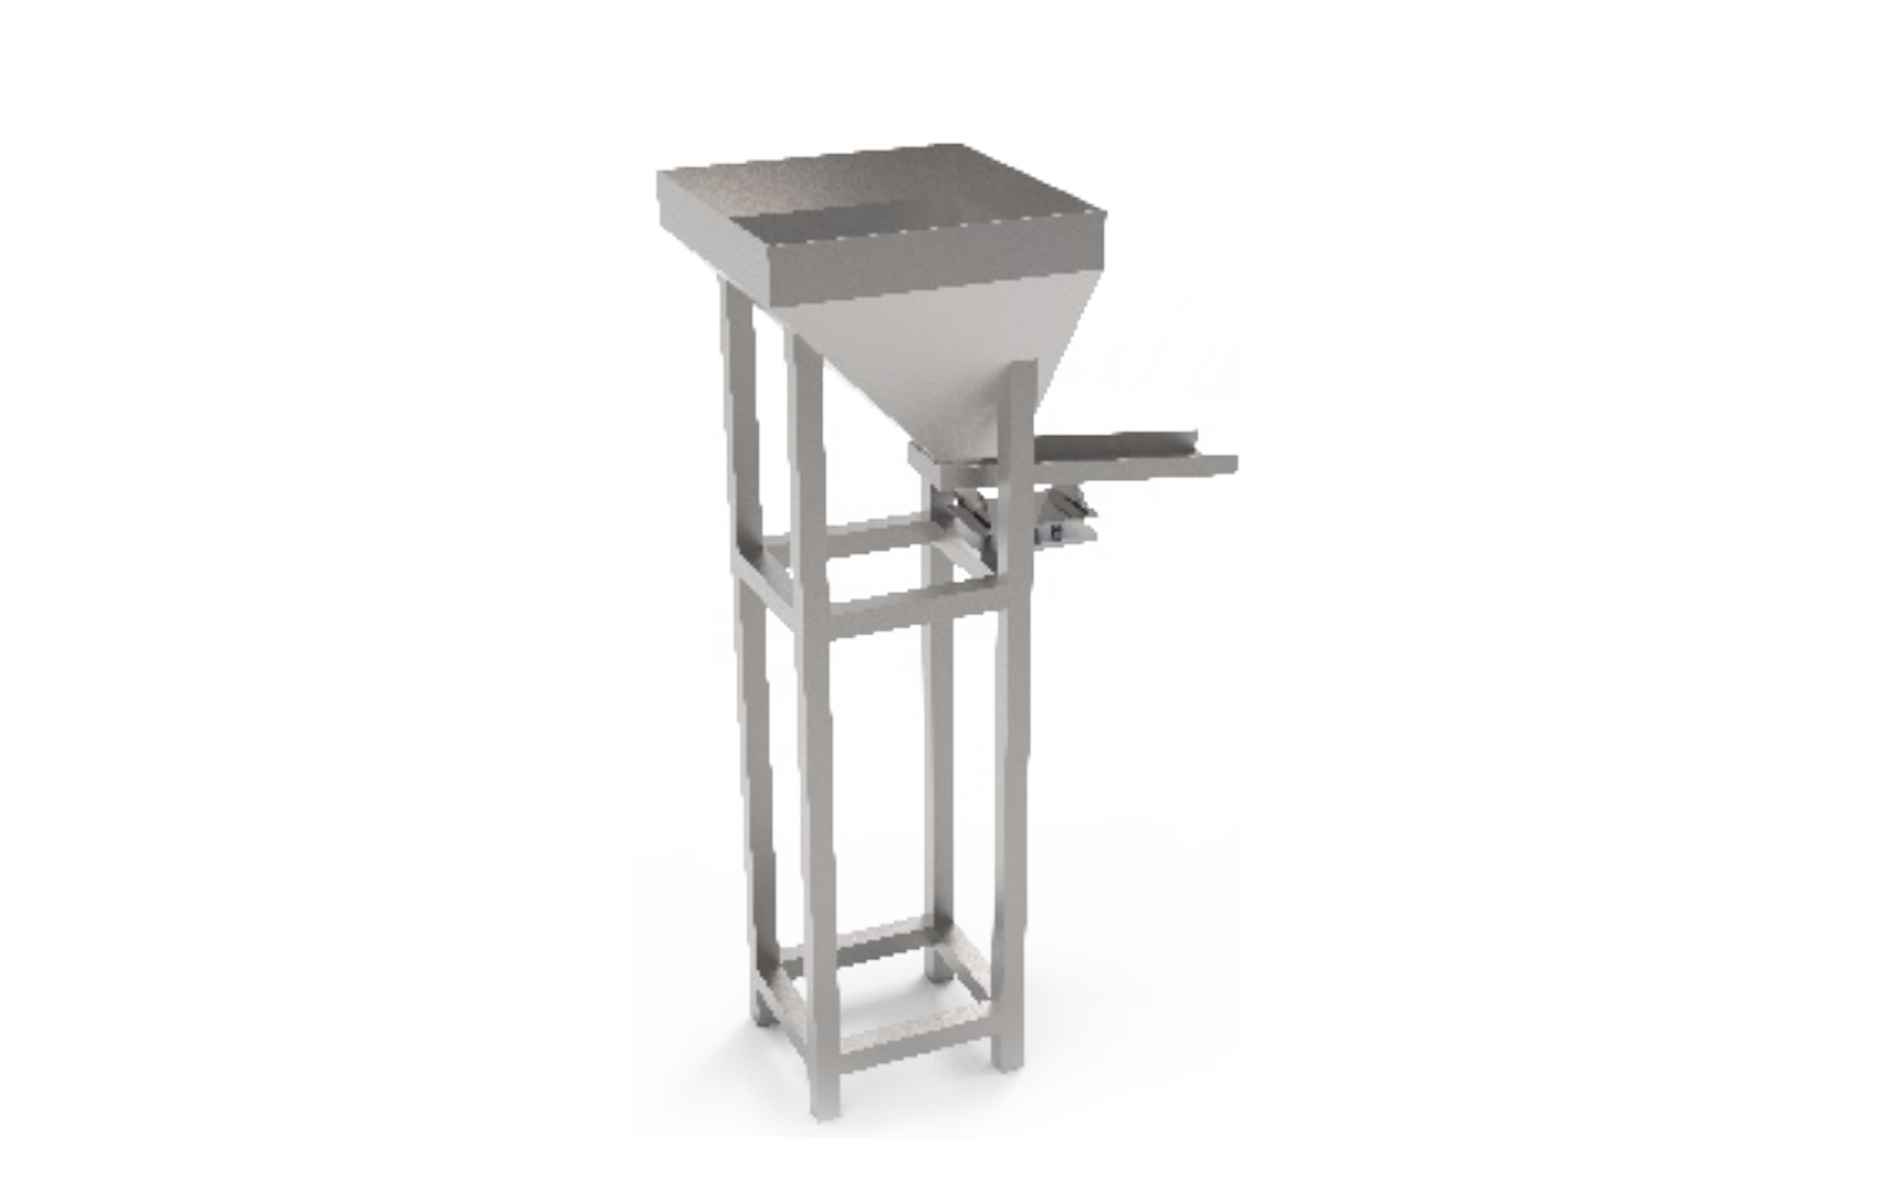
The materials are simply fed into the vibratory hopper. The hopper is mounted to special vibration motors or electromagnetic vibrators. When they are activated, they move in a controlled oscillation to transport material from the top of the hopper to the outlet.
Unlike gravity feeding systems, vibration feeding allows irregularly shaped products as well as fragile products to be transported without becoming stuck, while the amplitude of vibration and the feed rate are adjustable to switch between many different types of ingredient without changing the equipment.
Ingredients Vibratory Hopper can be used within several processing systems or modes:
It is particularly suitable for the transfer of grains and pulses, sugar, salt, spices, nuts and seeds, flour and snack foods, as it is gentle on the materials conveyed.
When combined with multi-head weighers, linear weighers and filling machines they can be used to provide a constant flow of ingredients for more accurate weighings.
Constant, uniform flow of ingredients minimizes line interruptions and maximizes line speed.
Automated feeding technologies are labor saving, improve workplace safety, and reduce costs.
The hopper has a constant supply of ingredients to provide a constant flow to ensure the mixing and weighing are accurate.
Controlled vibration prevents overfeeding, spillage, and loss of raw materials.
Its small size and modular design enable easy integration into existing processing and packaging lines.
Materials. Ingredients Vibratory Hoppers are typically made from SS 304 or SS 316 stainless steel that is corrosion resistant, durable, and adheres to food-safety standards. To prevent sticking and to allow easy cleaning, the inner surfaces of hoppers are usually polished or smoothened.
Hoppers may be fitted with optional extras such as dust covers, level sensors, discharge gates, and inspection ports, or may be mounted on frames, conveyors, or feeders. This movement increases the hoppers' versatility.
Modern vibratory hoppers can be equipped with variable frequency drives (VFDs) or electronic controllers to adjust and control the amplitude and frequency of the vibration to accommodate different types of ingredients or different speeds of production.
They are simple to communicate with PLCs, making them a key part of fully automatic production lines.
The type of feeding equipment you select can impact production levels, hygiene standards and product consistency. The Ingredients Vibratory Hopper provides a reliable, cost-effective and scalable solution for accurately dosing ingredients. Its ability to handle various materials, ease of cleaning and capability to run continuously makes it the modern factory's preferred method of conveyance.
Whether you operate a small processing facility or a large manufacturing plant, investing in a good quality vibratory hopper will mean more uptime, efficiency and output for your process.
The Ingredients Vibratory Hopper is a component of a collection of processes, designed to store and dispense bulk ingredients and materials whilst ensuring product flow consistency, optimal machine performance, and product quality in various applications. Its strong structure, adjustable feeding rate, and versatility make it an essential asset for industries requiring precision and performance, including food, pharmaceutical, chemical, and plastic industries.
With the addition of an Ingredients Vibratory Hopper to your production line, your automation systems will become more effective and more efficient at handling ingredients.