


Incline conveyor is a type of conveyor system used with the purpose of moving goods up and down surfaces with different elevations. Incline conveyors are an efficient way to transport and handle products. Incline conveyors are used in the food processing industry, food packaging industry, pharmaceutical industry, agriculture, mining industry, and the manufacturing industry. They can eliminate bottlenecks and lower labour costs.
Incline conveyors are a suitable form of equipment for moving bulk products and packages, as well as granules, powder and solid products. They can transport materials through multiple environments and can move heavy or fragile products, making them a versatile part of any production line system. Their adaptability makes them an excellent choice.
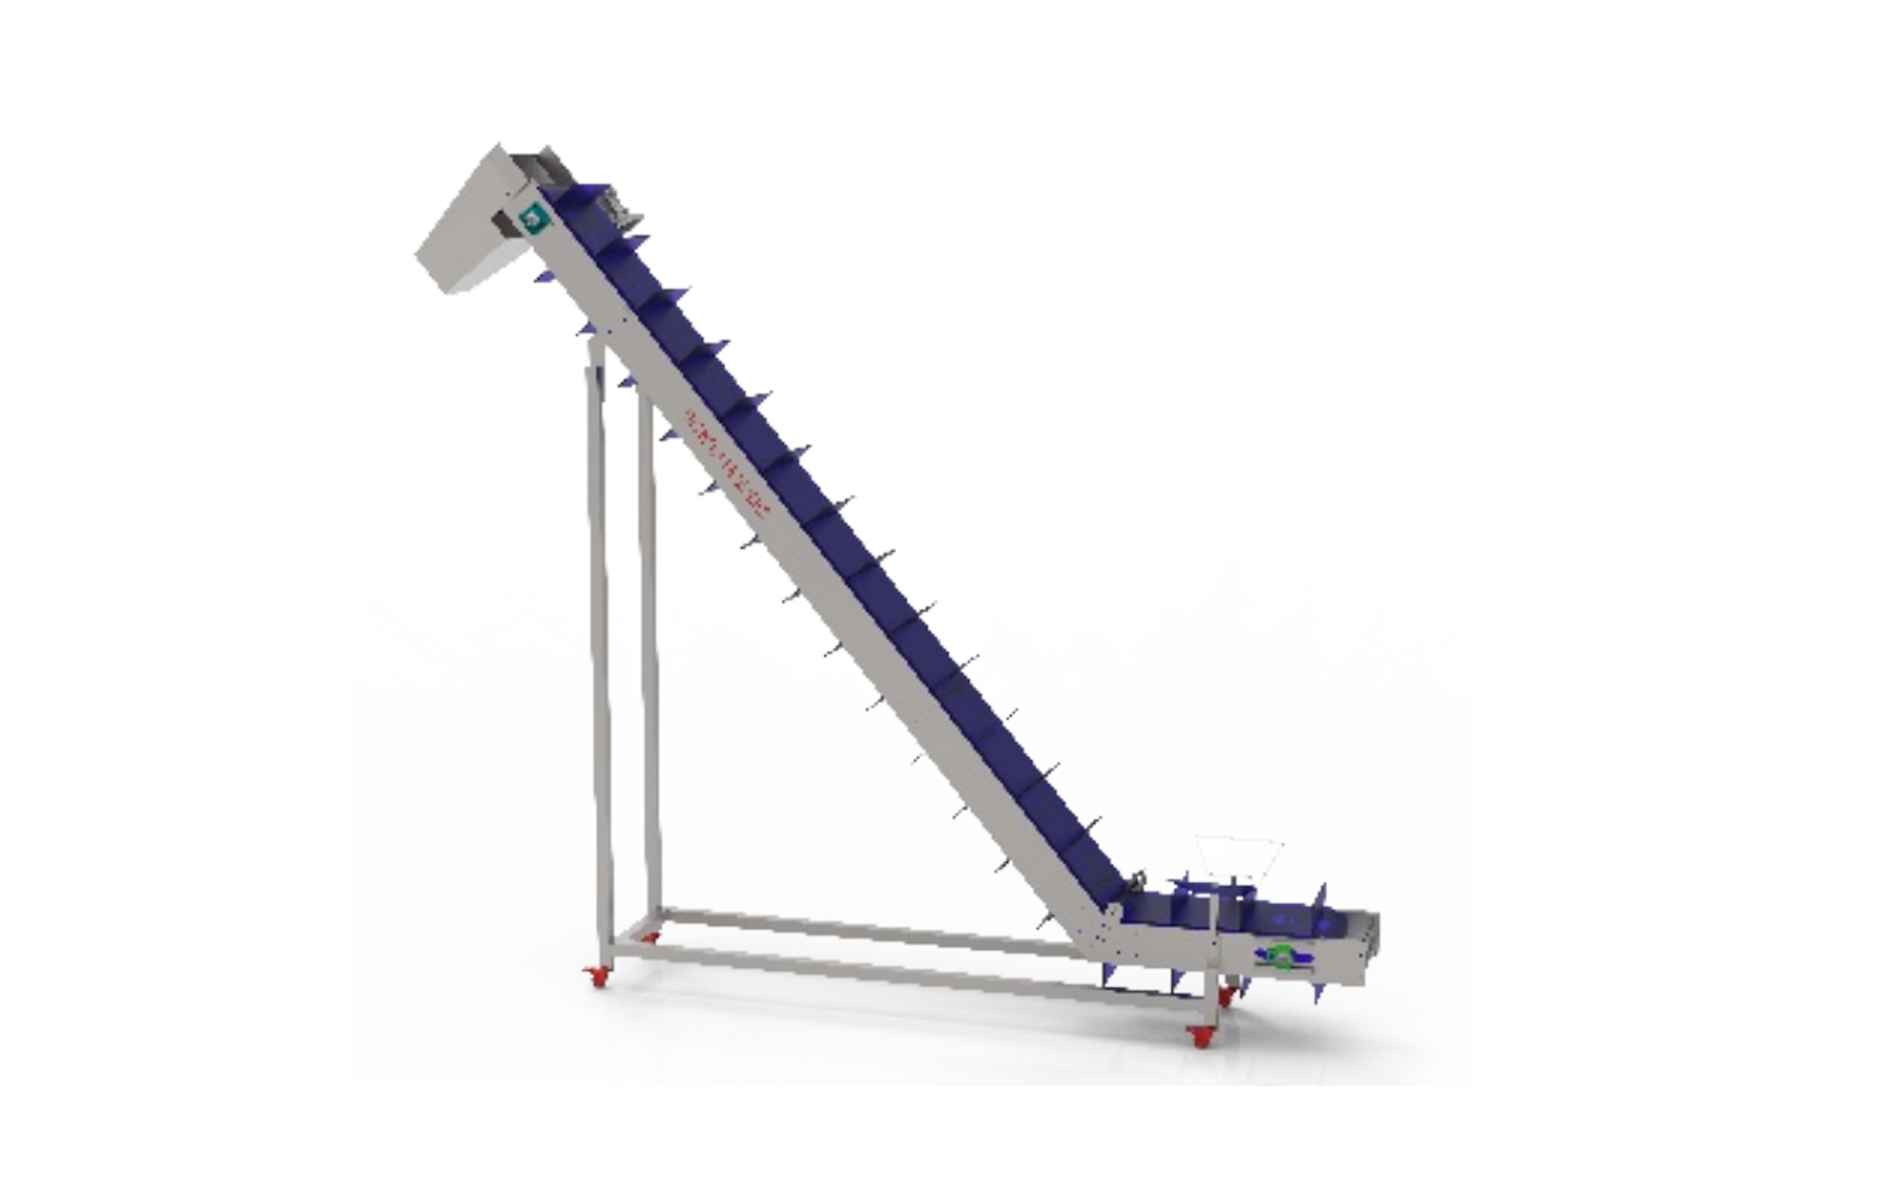
An Incline Conveyor is a mechanical conveyor used to move material to different elevations. Incline conveyors can be belted conveyor systems or modular conveyors, designed to ease upward and downward movement of materials, unlike flat belt conveyors that are meant to move material horizontally within the same level of a facility.
Incliners may include cleats, side walls or belts with high coefficients of friction to prevent product rollback, even at a steep angle of inclination. Incliners may have variable length, width, inclination angle, and be made of different materials according to the demands of the application.
Prominent features of incline conveyors include a straightforward construction and reliable operation. These include:
Incline conveyors can be designed in various configurations to suit the application and type of material:
This is used most commonly in shipping packed cargoes, cartons, boxes and packaged goods due to its continuous and reliable motion.
This type with vertical or inclined cleats is good for loose materials, grains, food products, or components that require more grip when being raised.
Modular plastic belts are built for food or sanitary applications where they can be cleaned and are more corrosion resistant.
These space-saving conveyors are also used for packaging and other automation applications where height transfer is required with a small footprint.
Installing an incline conveyor provides several operational and economic advantages:
Automated vertical transport saves labor time, and increases speed and throughput.
Incline conveyors make efficient use of vertical space and help with more organized facilities.
Helps reduce workplace injuries due to less need to manually lift and move heavy materials.
Ensures uninterrupted transfers, preventing spills and reducing product damage and waste.
It reduces labour and idle time, resulting in long-term savings.
Every production line is different, so incline conveyors can be customized to suit your specific needs. You can tailor the belt's width, length, angle of inclination, frame material, load capacity and motor power accordingly.
A high quality incline conveyor will give you a long service life with low maintenance and efficient operation. More so, if your operation has a continuous process, or high volume, it is well worth the investment.
Modern incline conveyors are used in combination with other machinery such as weighers, packaging machines, elevators or sorters, resulting in production being streamlined, automated and more productive, thus allowing the business to increase its throughput.
Incline Conveyors are versatile and effective, providing a dependable solution for the transportation of products from one level to another. Incline conveyors come in a variety of customizable designs and heavy-duty constructions, making them appropriate for applications in virtually every industry in modern material handling systems.
Whether you are upgrading equipment on an existing production line or building a new factory, an incline conveyor solution will provide the ideal package of performance, longevity and cost-effectiveness, allowing businesses to ensure a smooth operation and higher rates of production with minimum effort.